Heavy-duty epoxy systems for warehouses, retail, and industrial facilities — engineered for ROI and minimal downtime.
Compliant
Installs
Downtime kills profit. We install commercial-grade epoxy floors that protect your investment, reduce maintenance costs, and look professional for years. From food-safe USDA-compliant coatings to forklift-rated systems and ESD anti-static labs — we engineer the right system for your operation and install around your schedule.
Trowel-applied 1/4" thick — for impact zones, ramps, and heavy forklift staging areas. Urethane Cement
Thermal-shock resistant up to 250°F — perfect for kitchens and food processing.
Conductive primer and topcoat for electronics, server rooms, and sensitive labs.
Embedded color zoning for traffic lanes, walkways, and OSHA hazard markings.
Seamless wall-to-floor transitions — eliminates bacteria-harboring corners.
Forklift-rated epoxy mortar systems with safety striping for traffic lanes and pallet zones.
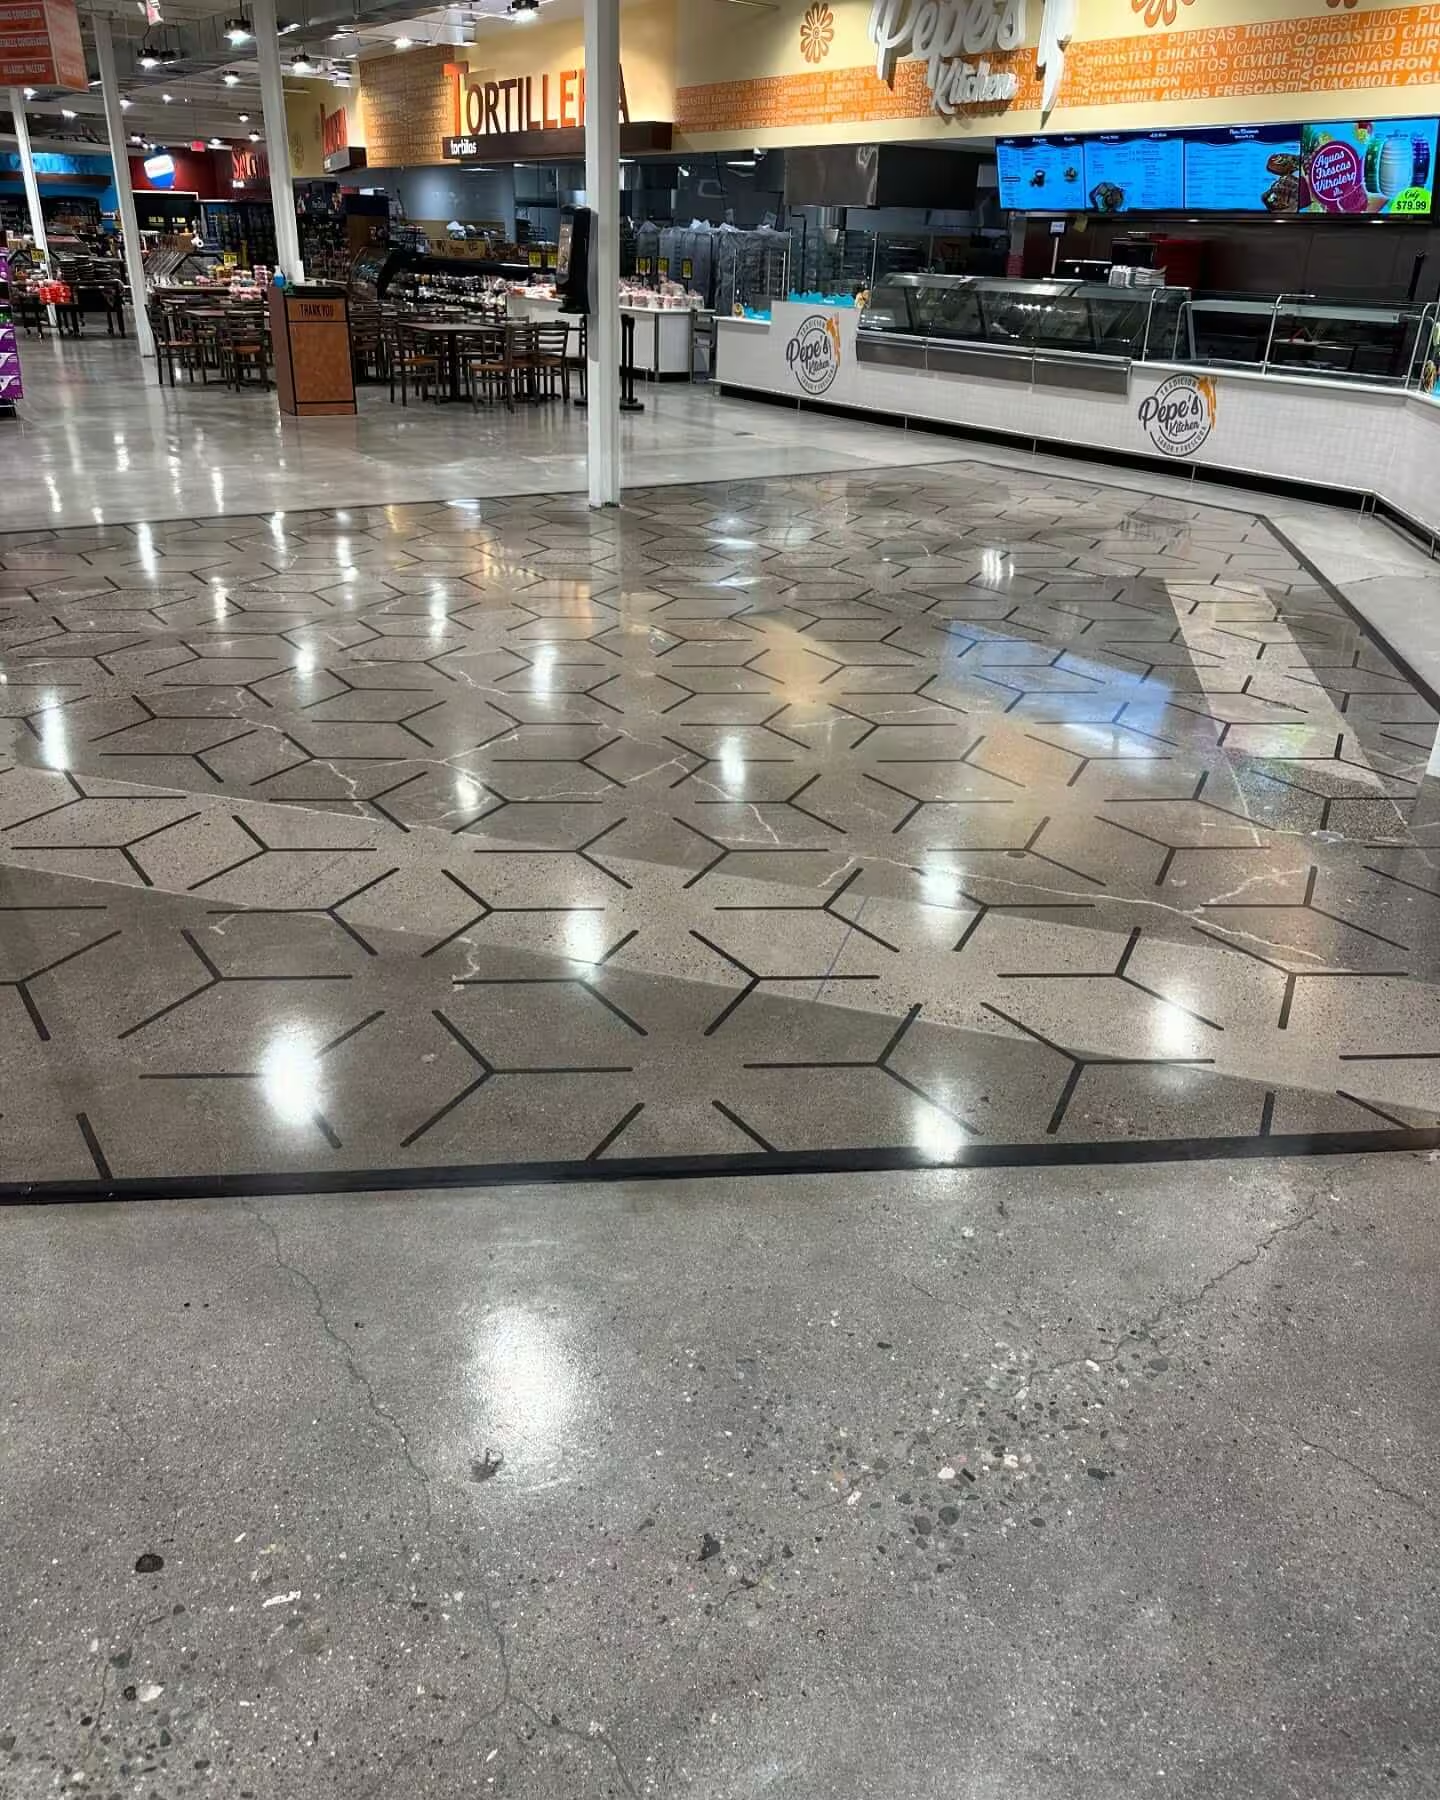
High-gloss decorative metallic epoxy that elevates your brand and showcases product.
USDA-compliant urethane cement — sanitary, slip-resistant, and thermal-shock resistant.
Chemical-resistant floors built for daily abuse from oil, brake fluid, and battery acid.
Acid- and sugar-resistant systems that handle wash-downs and hot liquids.
ESD anti-static and seamless cove-base systems for sensitive environments.